
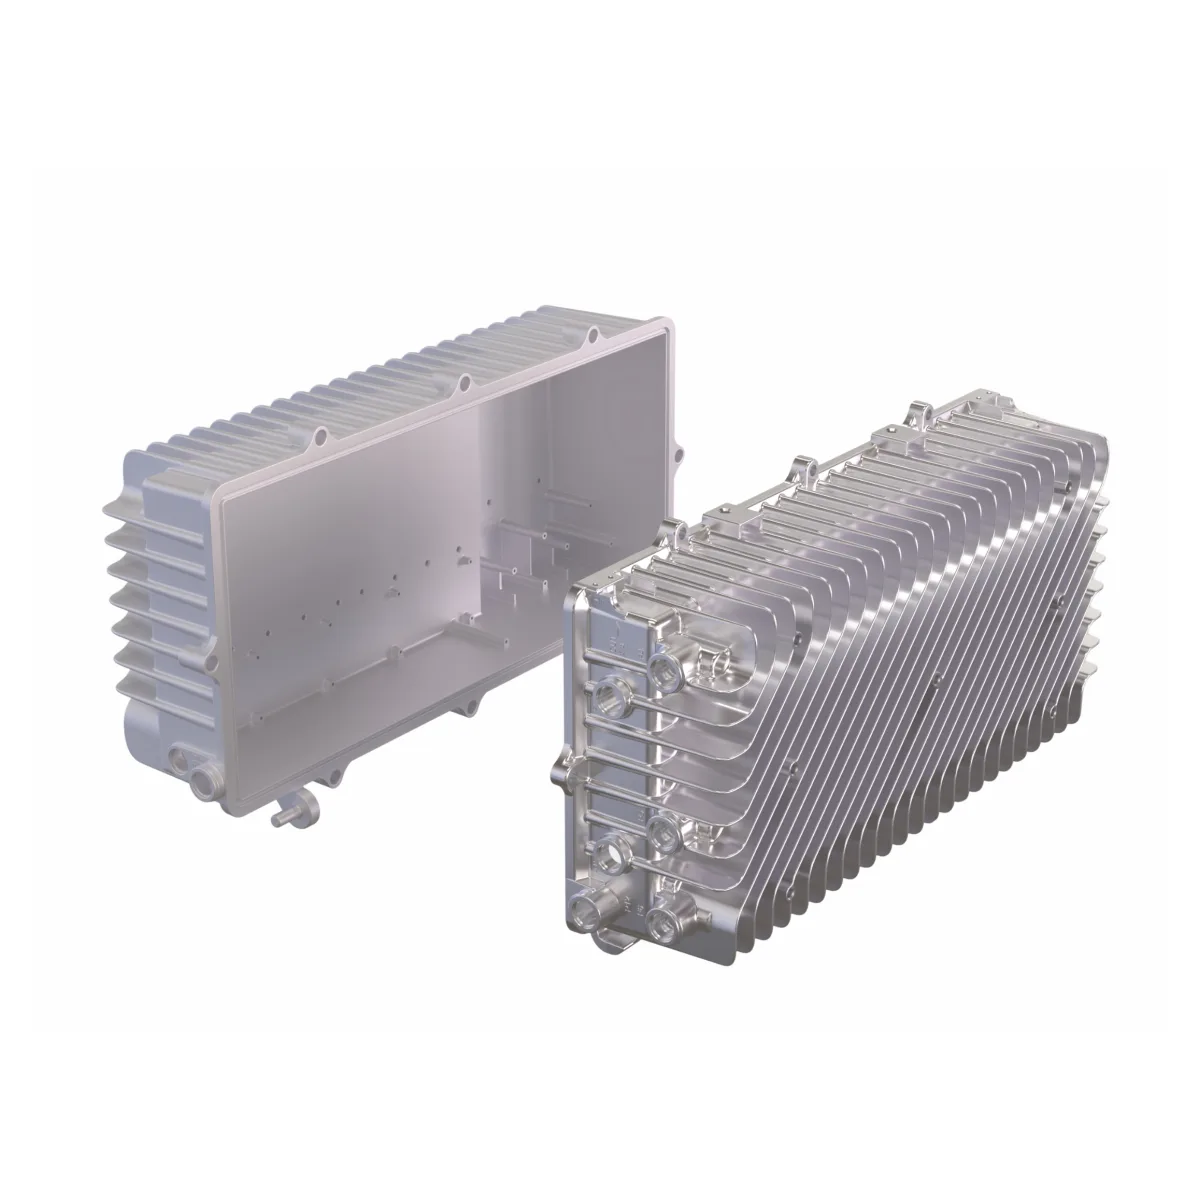
Zakázkové přesné díly
Vlastní 5G AAU masivní MIMO základnová stanice dutinový filtr hliníkový kryt a chladič
Custom aluminum die-cast & CNC 5G AAU cavity filter enclosure and heat sink. IP67 waterproof, PIM3 <= -160 dBc, handles 1800W TDP for Massive MIMO telecom base stations.
Výhody procesu a dodání
- Podporuje toleranci ±0,01 mm, s plným pokrytím 3/4/5osých CNC obráběcích center
- Materiály zahrnují hliníkovou slitinu, nerezovou ocel, měď, titanovou slitinu a konstrukční plasty
- V kombinaci s eloxováním, galvanickým pokovováním, nástřikem, laserovým gravírováním a dalšími povrchovými úpravami
- 100% úplná kontrola před odesláním, s poskytnutím zpráv o prvních kusech a rozměrových dat CP/CPK
- Vlastní kapacita v Dongguanu, 7-15 dní pro standardní díly, zrychlený kanál do 5 dnů
PŘEHLED PRODUKTU
Přehled produktu
Product Overview
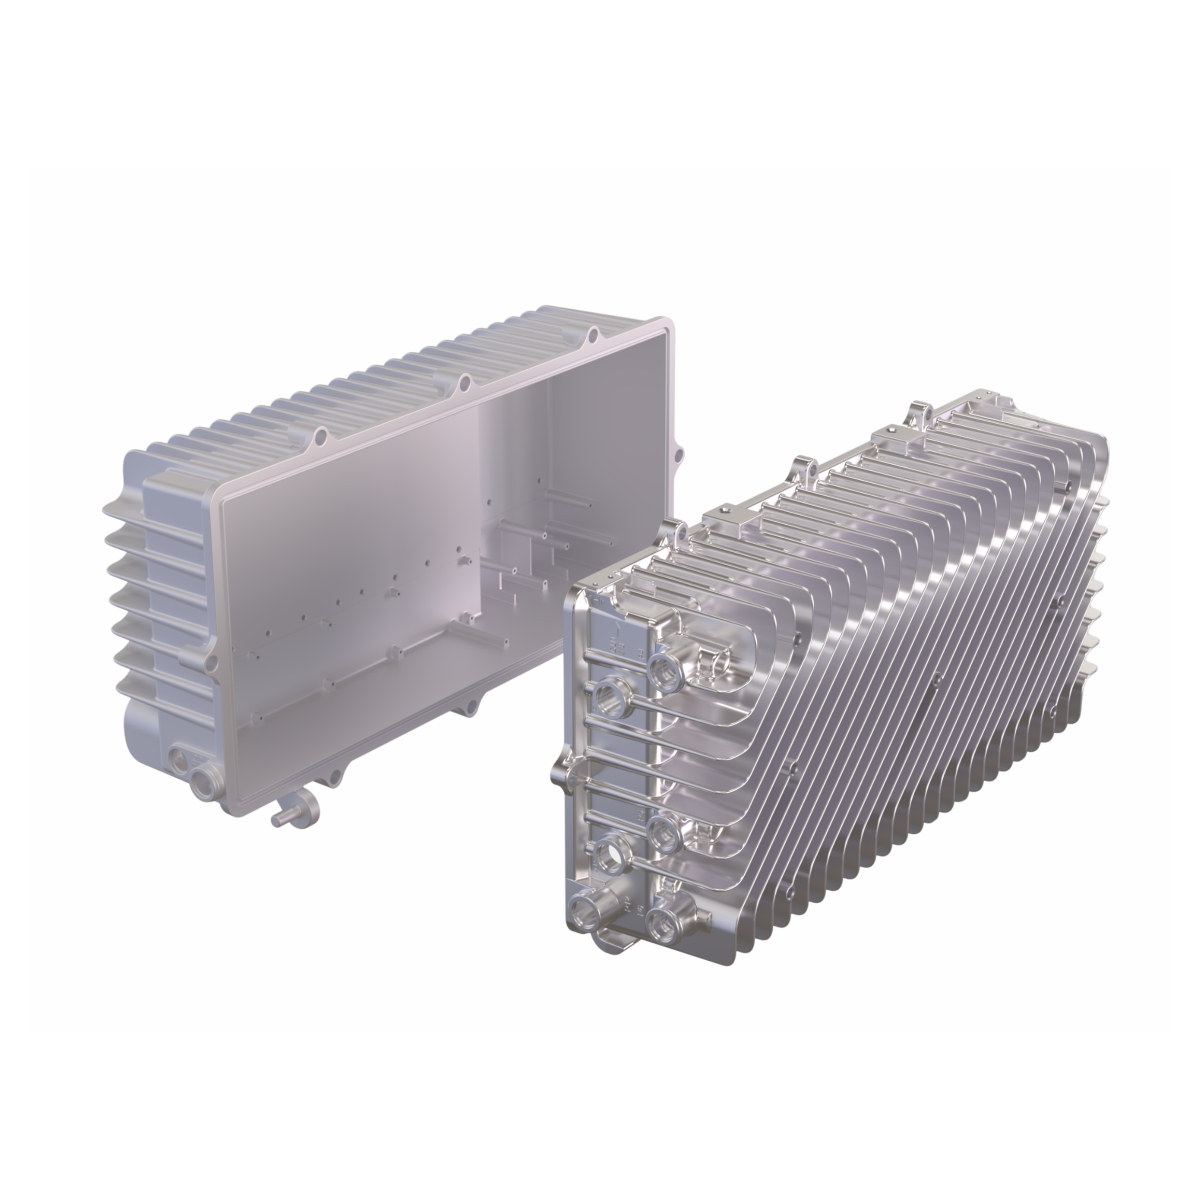
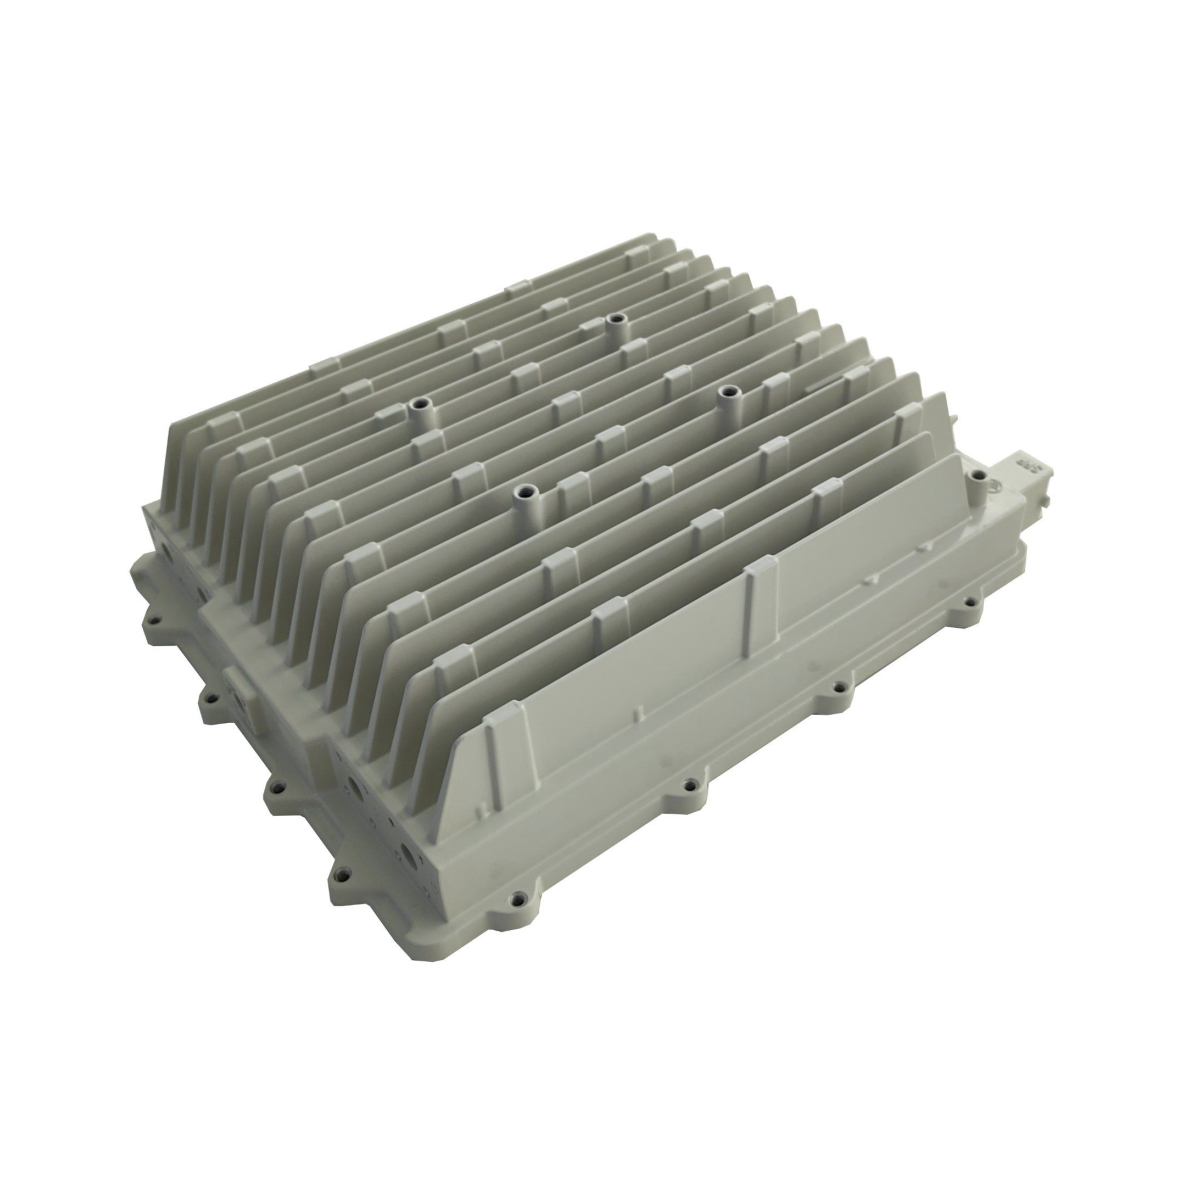
Engineered specifically for next-generation 5G Massive MIMO (32T32R, 64T64R) Active Antenna Units (AAU), Remote Radio Units (RRU), and outdoor micro-base stations, the Custom 5G AAU Cavity Filter Aluminum Enclosure & Heat Sink (Model: CP-5G-01) integrates precision RF filtering chambers and aerodynamic high-aspect-ratio thermal dissipation fins into a monolithic, weather-sealed aluminum structure.
By combining high-pressure semi-solid die casting (1600T~3500T) with multi-axis high-speed CNC milling (24,000 RPM diamond tool finishing), this enclosure eliminates multi-part interface thermal resistance while delivering extreme dimensional accuracy (±0.015 mm) across RF resonance cavities. Rated for continuous 800W~1800W GaN/LDMOS power amplifier heat loads, it achieves ultra-low passive intermodulation (PIM3 ≤ -160 dBc) and full IP67/IP68 ingress protection against severe outdoor environments.
Figure 1: Dual-Functional Monolithic Architecture — Precision Internal Cavity Resonance Chamber (Left) & Aerodynamic Cooling Fin Array with RF Port Feedthroughs (Right).
Technical Specifications
| Technical Parameter | Design Specification & Standard |
|---|---|
| Base Material Alloys | High-Thermal-Conductivity Die-Cast Aluminum (AlSi10Mg, ADC12, A380, A360) or Forged 6063-T6 / 6061-T6 |
| Primary & Secondary Processes | 1600T~3500T Semi-Solid Rheocasting + High-Speed 5-Axis CNC Milling (24,000 RPM) |
| Cavity Dimensional Tolerance | General: ±0.015 mm | Critical Resonance Cavity Depth: ±0.010 mm | Mounting Pitch: ±0.02 mm |
| Cavity Internal Surface Roughness | Ra ≤ 0.8 μm (Optimized to minimize RF skin-depth resistance and signal loss) |
| Passive Intermodulation (PIM3) | ≤ -160 dBc @ 2 × 43 dBm (Tested under vibration and thermal shock protocols) |
| Operating Frequency Bands | Sub-6 GHz (n77 / n78 / n79: 3.3 GHz ~ 4.9 GHz) & mmWave (24.25 GHz ~ 39 GHz) |
| Thermal Heat Flux Handling | 800W ~ 1800W+ continuous heat load | Thermal Resistance Rth ≤ 0.032 °C/W |
| Environmental Ingress Sealing | IP67 / IP68 Rated | Automated Form-in-Place (FIP) Conductive Silicone Gasket & O-Ring Groove |
| Corrosion Resistance & Surface Treatment | Cavity: Silver Plating (5~8 μm) / Tri-Metal Plating (Cu/Sn/Zn) | Exterior: SurTec 650 Passivation + Outdoor Powder Coat (≥ 1000h Salt Spray ASTM B117) |
RF Filtering & Thermodynamic Fin Architecture
Unlike traditional two-piece designs that bolt separate filter boxes onto an external heat sink, Altus Precision utilizes a monolithic dual-sided integration architecture:
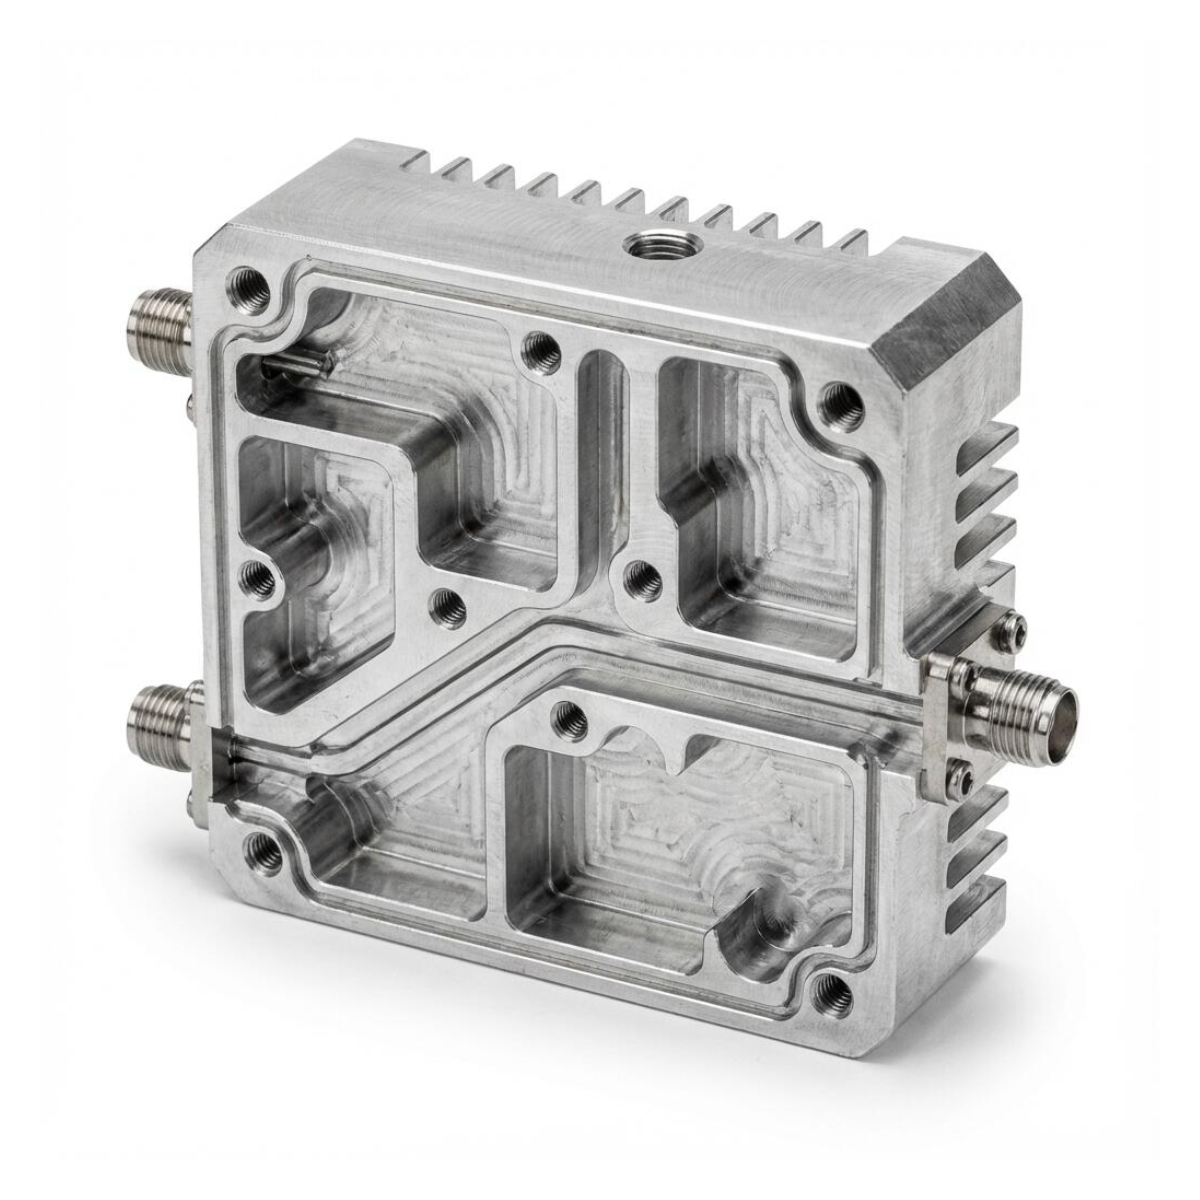
- Precision Multi-Cell Resonant Chambers (RF Front): Deep-cavity CNC milling forms isolated resonant cells separated by 1.2mm~2.0mm high-rigidity shielding walls, achieving > 80 dB inter-channel isolation. Integrated precision bosses support M2.5~M3.5 tuning screws and dielectric resonator pegs with 4H thread tolerance.
- High-Aspect Aerodynamic Cooling Fins (Thermal Rear): Features variable-thickness tapered fins with aspect ratios up to 14:1. The fin pitch is aerodynamically contoured to optimize both natural thermal buoyancy under dead-calm solar radiation and forced convective cooling in tower-mounted wind environments.
- Embedded Phase-Change Enhancement (Optional): For concentrated 200W+ GaN power amplifier hot spots, our engineering team can integrate vacuum-soldered copper-nickel heat pipes or micro vapor chambers (VC) directly into the die-cast baseplate for rapid planar heat spreading.
Precision CNC milled RF filter cavities with SMA coaxial ports & Ra ≤ 0.8 μm mirror finish.
High-aspect-ratio aerodynamic cooling fins and mounting boss array on weather-sealed chassis.
Metallurgy & Manufacturing Workflow
- Semi-Solid Rheocasting (1600T~3500T): Utilizing globular microstructures at solid-liquid coexistence states, achieving dense, pore-free internal castings (< 0.8% gas porosity, ASTM E505 Class 1 rating) that prevent RF micro-discharge.
- 5-Axis High-Speed CNC Roughing & Finishing: Multi-axis positioning handles complex 3D contours, O-ring gasket retention grooves, coaxial feedthrough holes, and precision cavity depths in single setups to eliminate datum shift errors.
- Robotic Form-in-Place (FIP) Dispensing: Automated micro-dispensing of nickel-graphite conductive silicone gaskets directly into the CNC milled perimeter groove for IP67 water sealing and > 90 dB EMI shielding.
- Surface Plating & Environmental Passivation: Electroless copper strike followed by 5~8 μm ultra-pure silver or white bronze plating in RF resonant regions; SurTec 650 hexavalent-chromium-free passivation on external faces followed by 80~120 μm weather-resistant electrostatic polyester powder coating.
Quality Inspection & Telcordia Reliability Protocols
- 3D CMM Full-Cavity Metrology: Zeiss Coordinate Measuring Machines inspect critical cavity depths, wall positions, and bolt hole centers against 3D CAD step files with ±0.01mm measurement resolution.
- PIM & RF S-Parameter Verification: Keysight vector network analyzers and dedicated PIM test benches verify insertion loss, return loss, and third-order intermodulation (≤ -160 dBc @ 2 × 43 dBm) under dynamic mechanical vibration.
- IP67/IP68 Air-Tightness Decay Test: 100% of finished enclosures undergo differential pressure vacuum decay testing (ΔP ≤ 20 Pa over 60 seconds, equivalent leak rate < 0.02 cc/min).
- Telcordia GR-487 Environmental Compliance: Qualified under cyclic thermal shock (-40 °C to +125 °C, 1000 cycles), 1000-hour neutral salt spray (ASTM B117), and 50g mechanical shock tests.
Frequently Asked Questions (FAQs)
Q1: How does Altus Precision achieve ultra-low PIM (PIM3 ≤ -160 dBc) in die-cast aluminum cavity filters?
A: Low PIM performance requires strict elimination of ferromagnetic contaminants, micro-cracks, and galvanic junctions. We utilize high-purity virgin aluminum ingots, vacuum semi-solid casting to eliminate internal pores, high-speed diamond tooling for mirror-smooth cavity walls (Ra ≤ 0.8 μm), ultra-pure silver/tri-metal plating, and non-magnetic stainless steel threaded inserts (SUS304/SUS316).
Q2: Can the cavity filter housing integrate heat pipes or vapor chambers for 1500W+ GaN amplifiers?
A: Yes. For high-power 5G Massive MIMO AAUs with concentrated heat flux (≥ 50 W/cm²), we routinely embed sintered copper heat pipes or composite aluminum-copper vapor chambers into the baseplate using precision CNC slotting and vacuum flux-free soldering, ensuring thermal impedance below 0.025 °C/W.
Q3: What outdoor environmental and weatherproofing ratings are certified?
A: The enclosure is certified for IP67 and IP68 outdoor deployment per IEC 60529. It passes 1000 hours of continuous neutral salt spray testing (ASTM B117), UV accelerated weathering (ASTM G154), and Telcordia GR-487 wind-driven rain and cyclic humidity standards without blistering or corrosion.
Q4: What are the typical lead times and DFM review procedures for custom 5G enclosures?
A: Upon receiving 3D CAD models (STEP/IGES/Parasolid), our engineering team completes comprehensive DFM, mold-flow, and thermal simulation reports within 24–48 hours. Functional rapid-prototype samples milled from solid aluminum billet ship in 10–12 business days, while production die-casting tooling and first-article qualification take 25–30 days.
SOUVISEJÍCÍ PRODUKTY
Související produkty
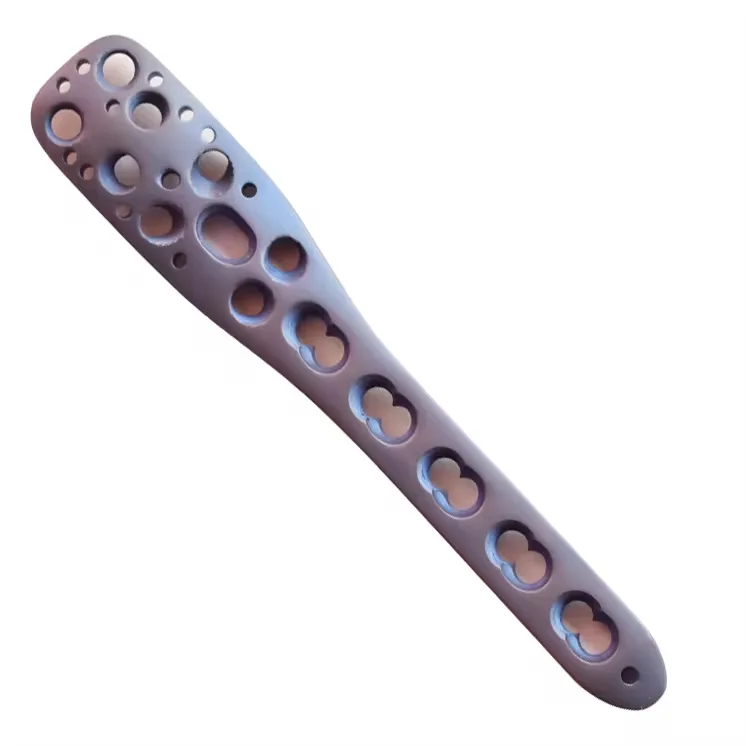
Zakázkové 5osé CNC titanové femorální uzamykací dlahy a maxilofaciální implantáty (OEM ukázka)
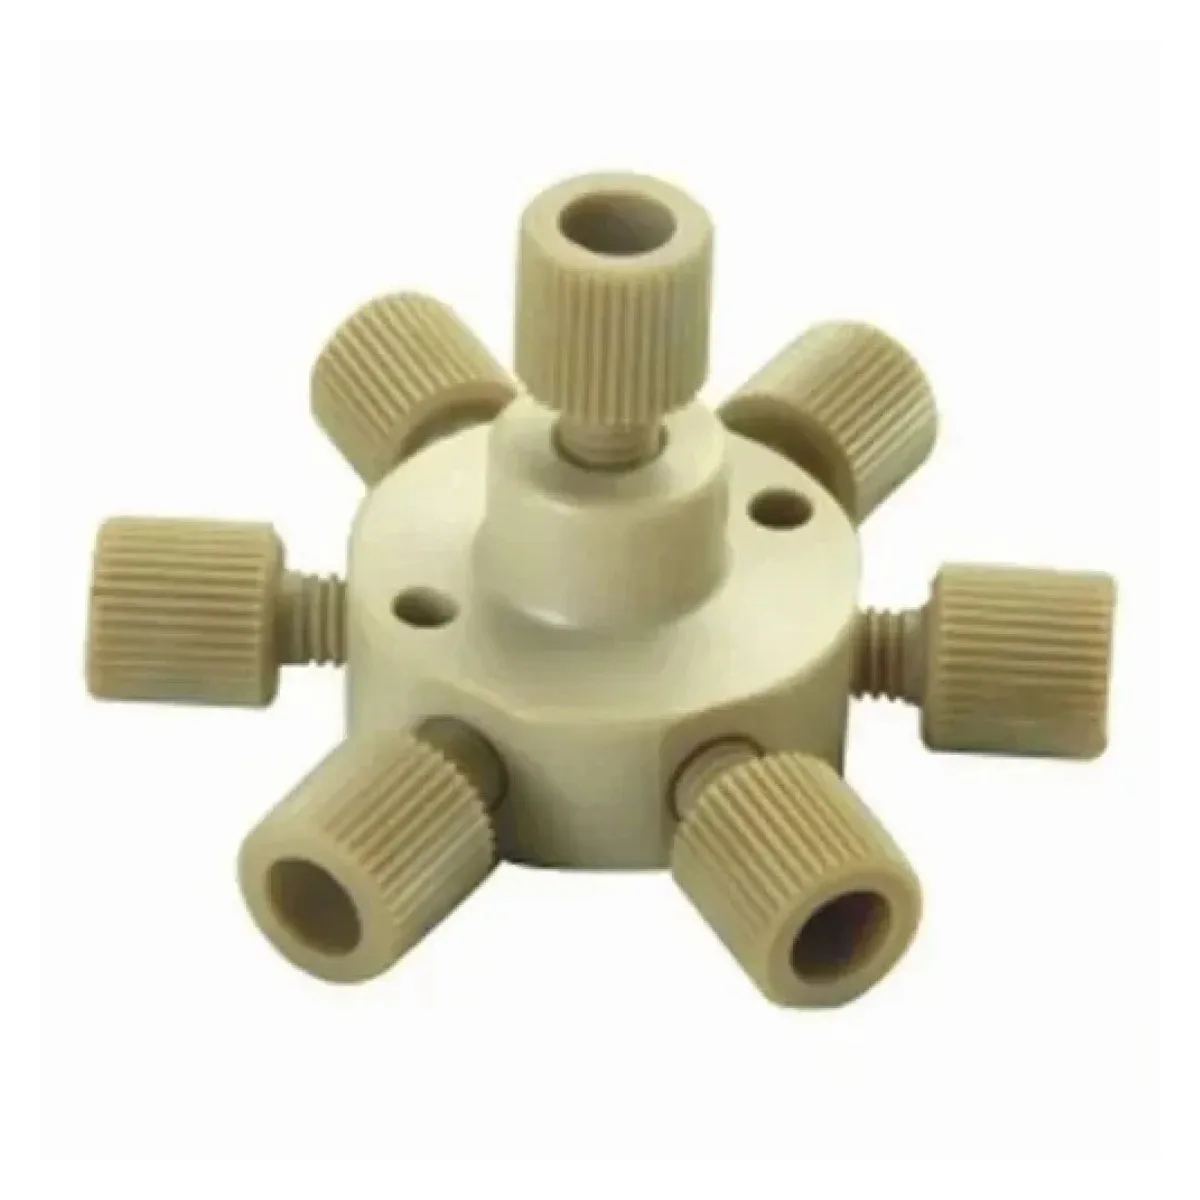
Zobrazit detaily →Zakázkový PEEK a 316L nerezový ocelový přesný fluidní rozvodný blok ventilu pro HPLC
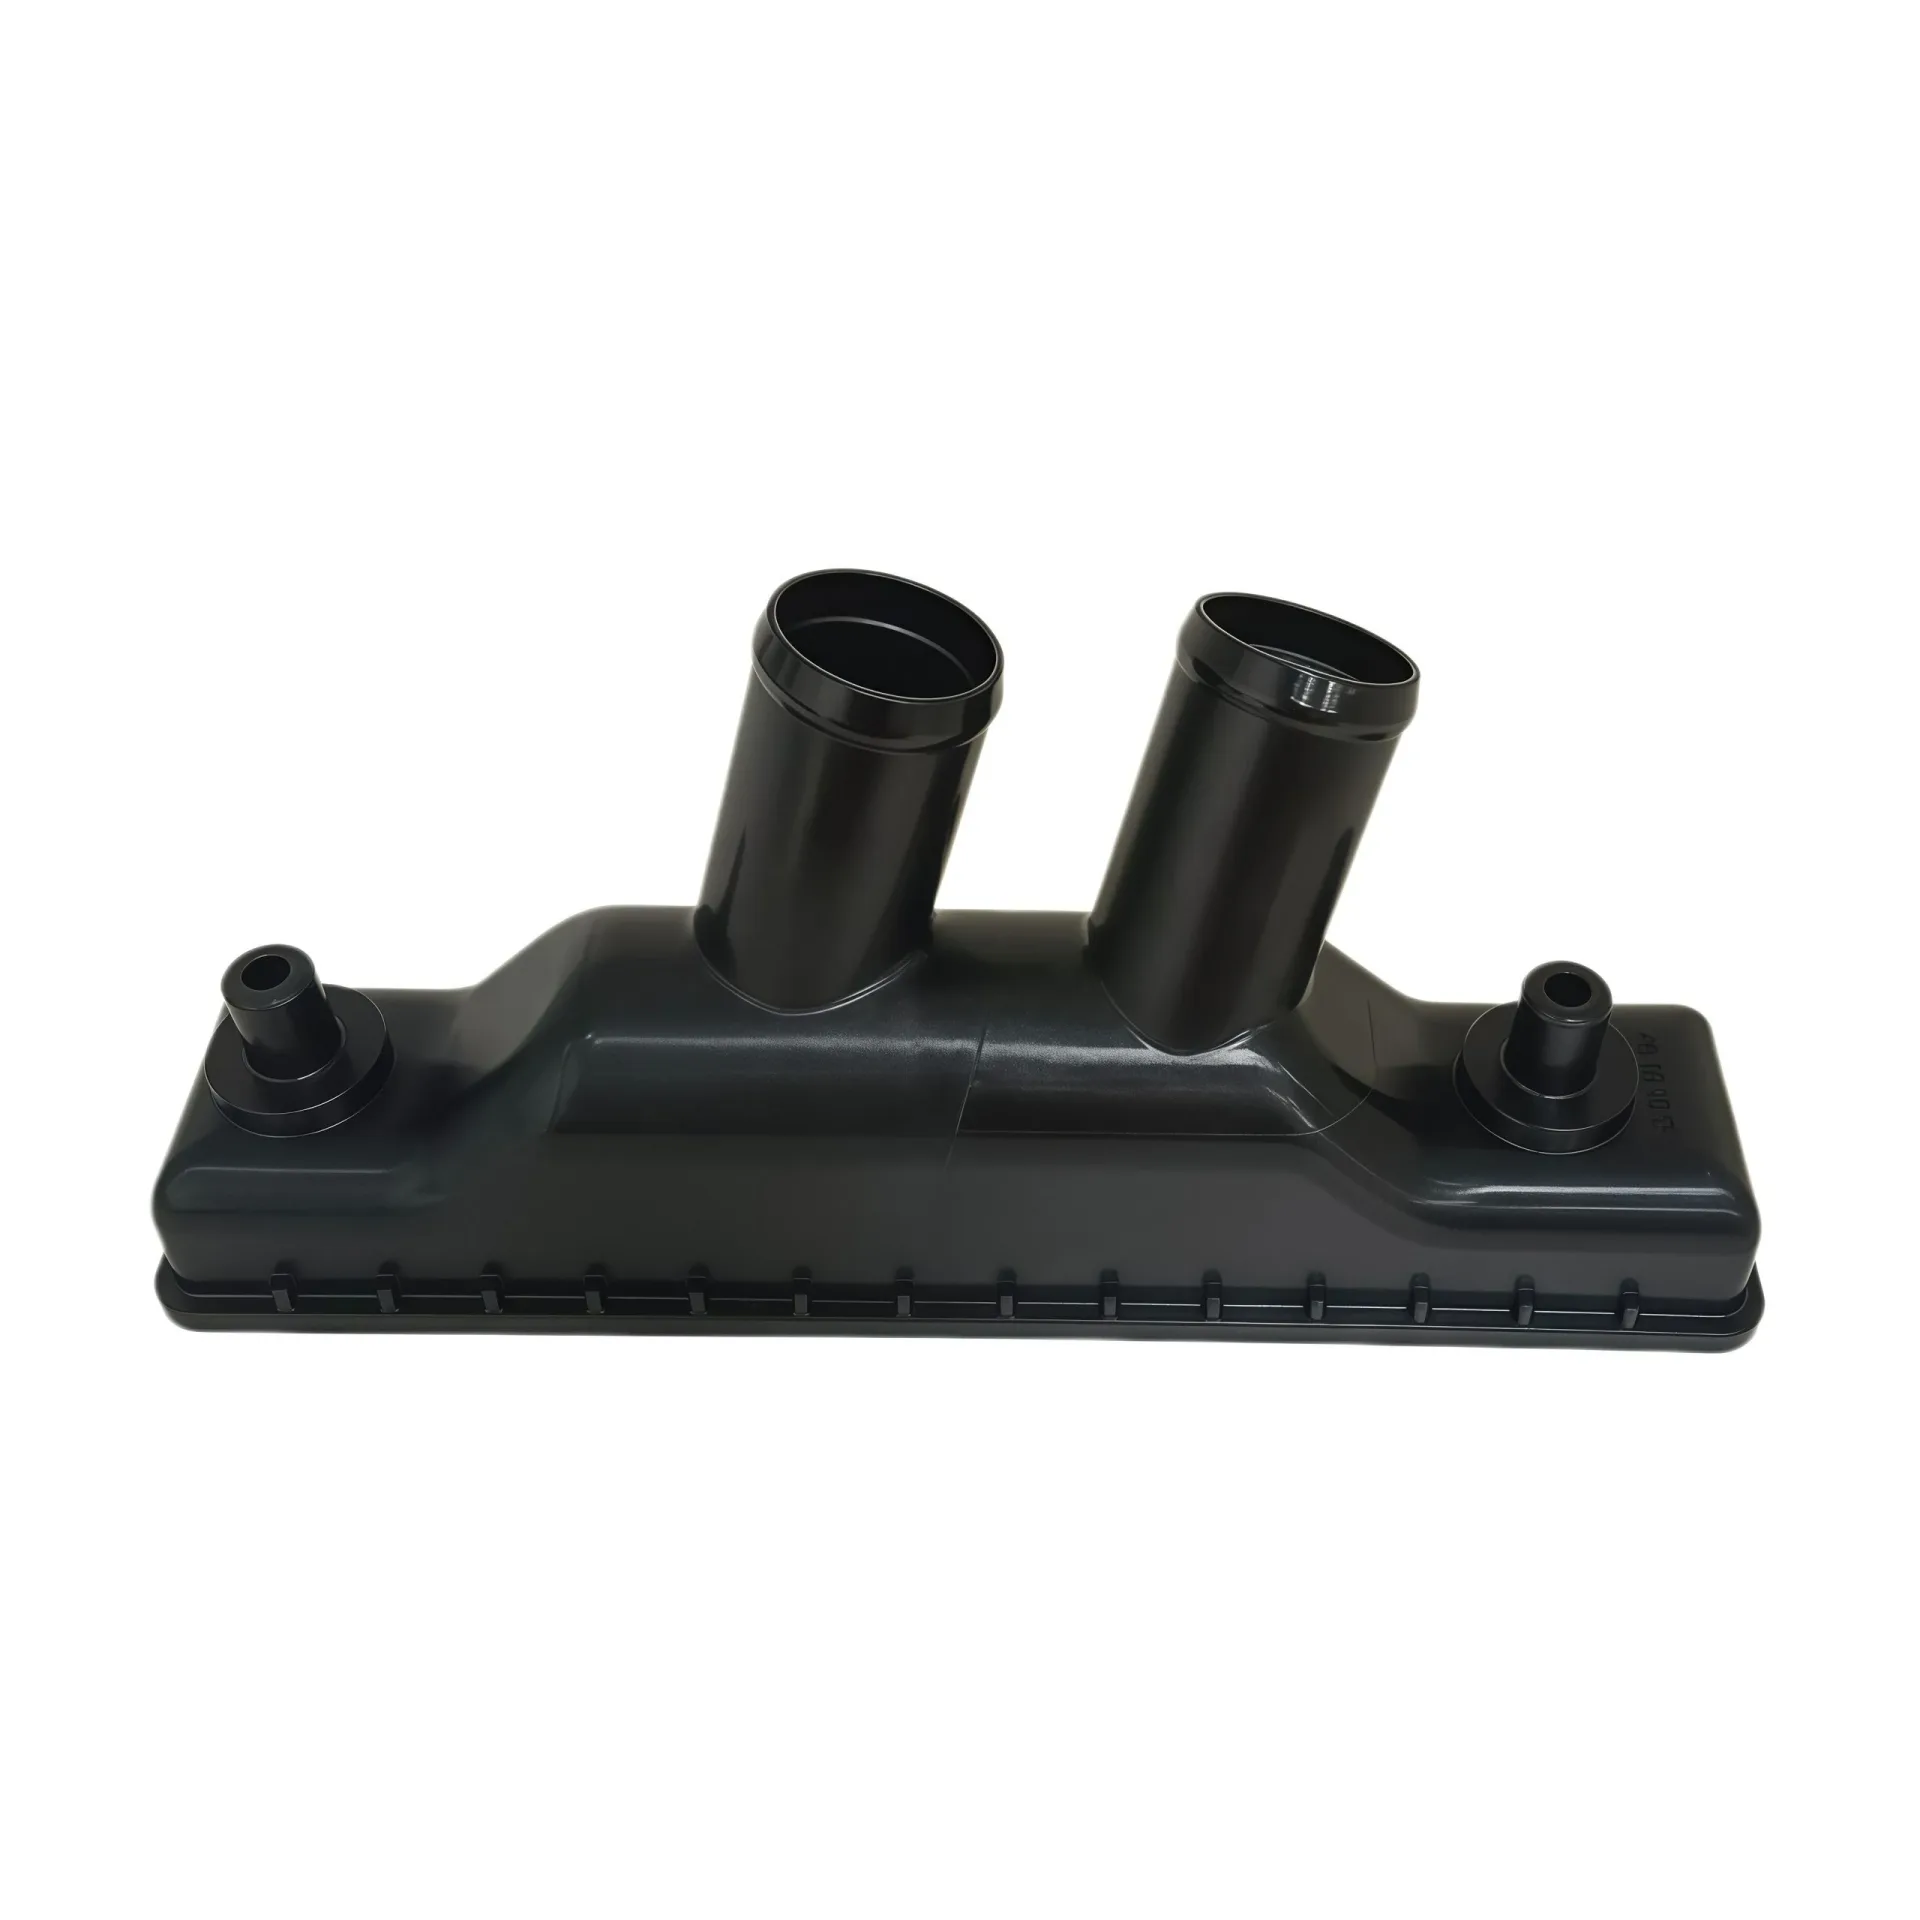
Zobrazit detaily →Vlastní plastový komponent chladicího potrubí pro automobily z materiálu PA66 GF30
Zobrazit detaily →Vlastní měděná trubka integrovaná v hliníkovém deskovém kapalinovém chladiči
Zobrazit detaily →Odeslat poptávku
Sdělte nám své výkresy, množství a požadavky na dodání. Náš technický tým odpoví s technologickým plánem a cenovou nabídkou do 24 hodin.
E-mailinfo@altusprecision.com
Telefon+86 13418313631
WhatsApp+86 13418313631
AdresaDongguan, Guangdong, Čína