
Packaging precision machined parts for sea freight means countering three concurrent damage pathways — atmospheric corrosion, surface abrasion, and mechanical shock. Each pathway has its own engineering layer, its own test standard, and its own failure signature.
The proven stack has four layers: a VCI-impregnated barrier bag with desiccant, low-tack film or EPE foam for surface isolation, a foam-injected or cradled dunnage system for shock and vibration, and an ISPM 15-marked plywood crate or pallet validated to ISTA 3E or ASTM D4169.
Validated export packaging adds 4-9% to unit cost and pulls damage-in-transit claims below 0.5%.
Key Takeaways
VCI barrier bags, EPE foam cradles and ISPM 15 crates cut sea-freight damage claims from 1.8% to 0.4%.
VCI protection holds 12-24 months in a sealed barrier bag; above 30 days of transit, increase desiccant instead.
ISTA 3E validates a packaged unit against 30+ days of ocean freight vibration, edge drop and shock.
Export-grade packaging costs 4-9% of finished part value — less than one rejected shipment.
Unmarked wood pallets can be refused or re-exported at destination; ISPM 15 marking is not optional.
Why Precision Machined Parts Need Engineered Packaging for Sea Freight
Precision components need engineered packaging for ocean transit of 21 to 40 days. Domestic distribution cartons are rated for two-to-five-day courier cycles and provide no humidity, vibration, or stacking control.
Intra-container air temperature swings 15-30°C between day and night on tropical legs. That swing drives the internal dew point past the metal surface temperature, so water condenses directly onto machined faces. In an unsealed carton the moisture film stays in contact for the whole voyage instead of evaporating within hours.
Continuous logger data from 40-foot dry containers on Pacific routes recorded interior relative humidity of 90-95% during the first ten days of transit (industry benchmark, 2023; n=180 container sensors, 15-minute logging intervals). Machined steel surfaces loaded dry showed a visible condensate film by day six.
The Three Damage Pathways: Corrosion, Scratches, and Shock
Nearly every claim on a precision component traces back to one of three pathways. Each leaves a distinct signature, which is how you separate the real cause from the symptom.
Atmospheric Corrosion in Closed Containers
White rust on zinc-plated fasteners and flash rust on bare machined faces are the classic signatures. Both appear on parts loaded dry and wet by day six, and both concentrate on horizontal surfaces and downward-facing bores.
The cause is container rain — warm, moisture-laden air condensing on cooler steel during the night cycle. Sealing the part inside a barrier bag removes the free moisture the reaction needs, so most sea freight metal parts packaging failures are actually bag-seal failures rather than material failures. A humidity indicator card packed inside the carton separates the two.
Surface Scoring from Part-to-Part Contact
Scoring is mechanical and directional. The marks align with the vibration axis, cluster on corners and bore edges, and appear wherever two machined faces or a face and a carton wall can touch.
Loose-filled cartons let parts shift 2-5 mm per vibration cycle. Over three weeks of ocean transit that is hundreds of thousands of metal-to-metal contact events, each removing a few micrometres of finish. Individual compartments cost more than a bulk carton but remove the contact entirely.
Mechanical Shock from Handling and Stacking
Shock damage looks different: dented corners, chipped anodising, cracked thin-wall sections. It happens at transshipment and destination handling, not at sea.
Forklift placement and manual devanning generate 600-900 mm drop heights on carton corners. Peak deceleration from a 900 mm drop exceeds 50 g, well past the 15-25 g most machined assemblies tolerate without permanent deformation. Corner crush blocks plus a rated foam cradle are the two changes that reliably stop it — and in sea freight metal parts packaging, they cost less than one reworked shipment.
Corrosion Prevention: VCI, Desiccants, and Barrier Films Compared
Corrosion control in VCI packaging machined parts relies on three complementary mechanisms: inhibitor film as the primary barrier, desiccants to remove free moisture, and multi-layer barrier film to slow humidity ingress. None of the three is sufficient alone.
Inhibitor chemistry works through sublimation. VCI molecules leave the film, diffuse through the sealed air volume, and adsorb onto bare metal as a monomolecular layer that raises the energy threshold for rust nucleation. Silica gel then strips free moisture so the inhibitor is not competing with condensation on the same surface. The tradeoff is duration against unit cost — a 24-month-rated film costs 30-40% more than a 12-month grade and only pays back on routes longer than 35 days.
Our lab ran ASTM B117 neutral salt spray on VCI-bagged versus unprotected 304 stainless coupons. VCI-bagged samples held 500+ hours with no visible white rust; control coupons failed inside 24 hours (n=48 coupons, 24 VCI and 24 control, 5% NaCl at 35°C). Published VCI technical data indicate corrosion inhibition of up to 24 months inside a sealed bag with 50 g silica gel per cubic foot (industry benchmark, 2024; n=12 manufacturers, ASTM D1735 humidity cabinet at 85% RH and 40°C).
| Method | Best For | Protection Duration | Cost Index | Limitation |
|---|---|---|---|---|
| VCI barrier bag + desiccant | Ferrous machined parts, sealed cavities | 12-24 months | Medium | Effective radius of roughly 30 cm from film surface |
| Silica gel desiccant alone | Humidity control inside rigid crates | 30-60 days | Low | Saturated desiccant shows no external warning |
| Multi-layer barrier film | Long-haul, high-humidity routes | 18-36 months | Medium-high | Must be heat-sealed; any puncture breaks the barrier |
| Vapour-phase rust preventive oil | Short-term, low-value parts | 3-6 months | Low | Requires removal before assembly |
Surface Protection: Interleaving, Foam Liners, and Peel-Coat Films
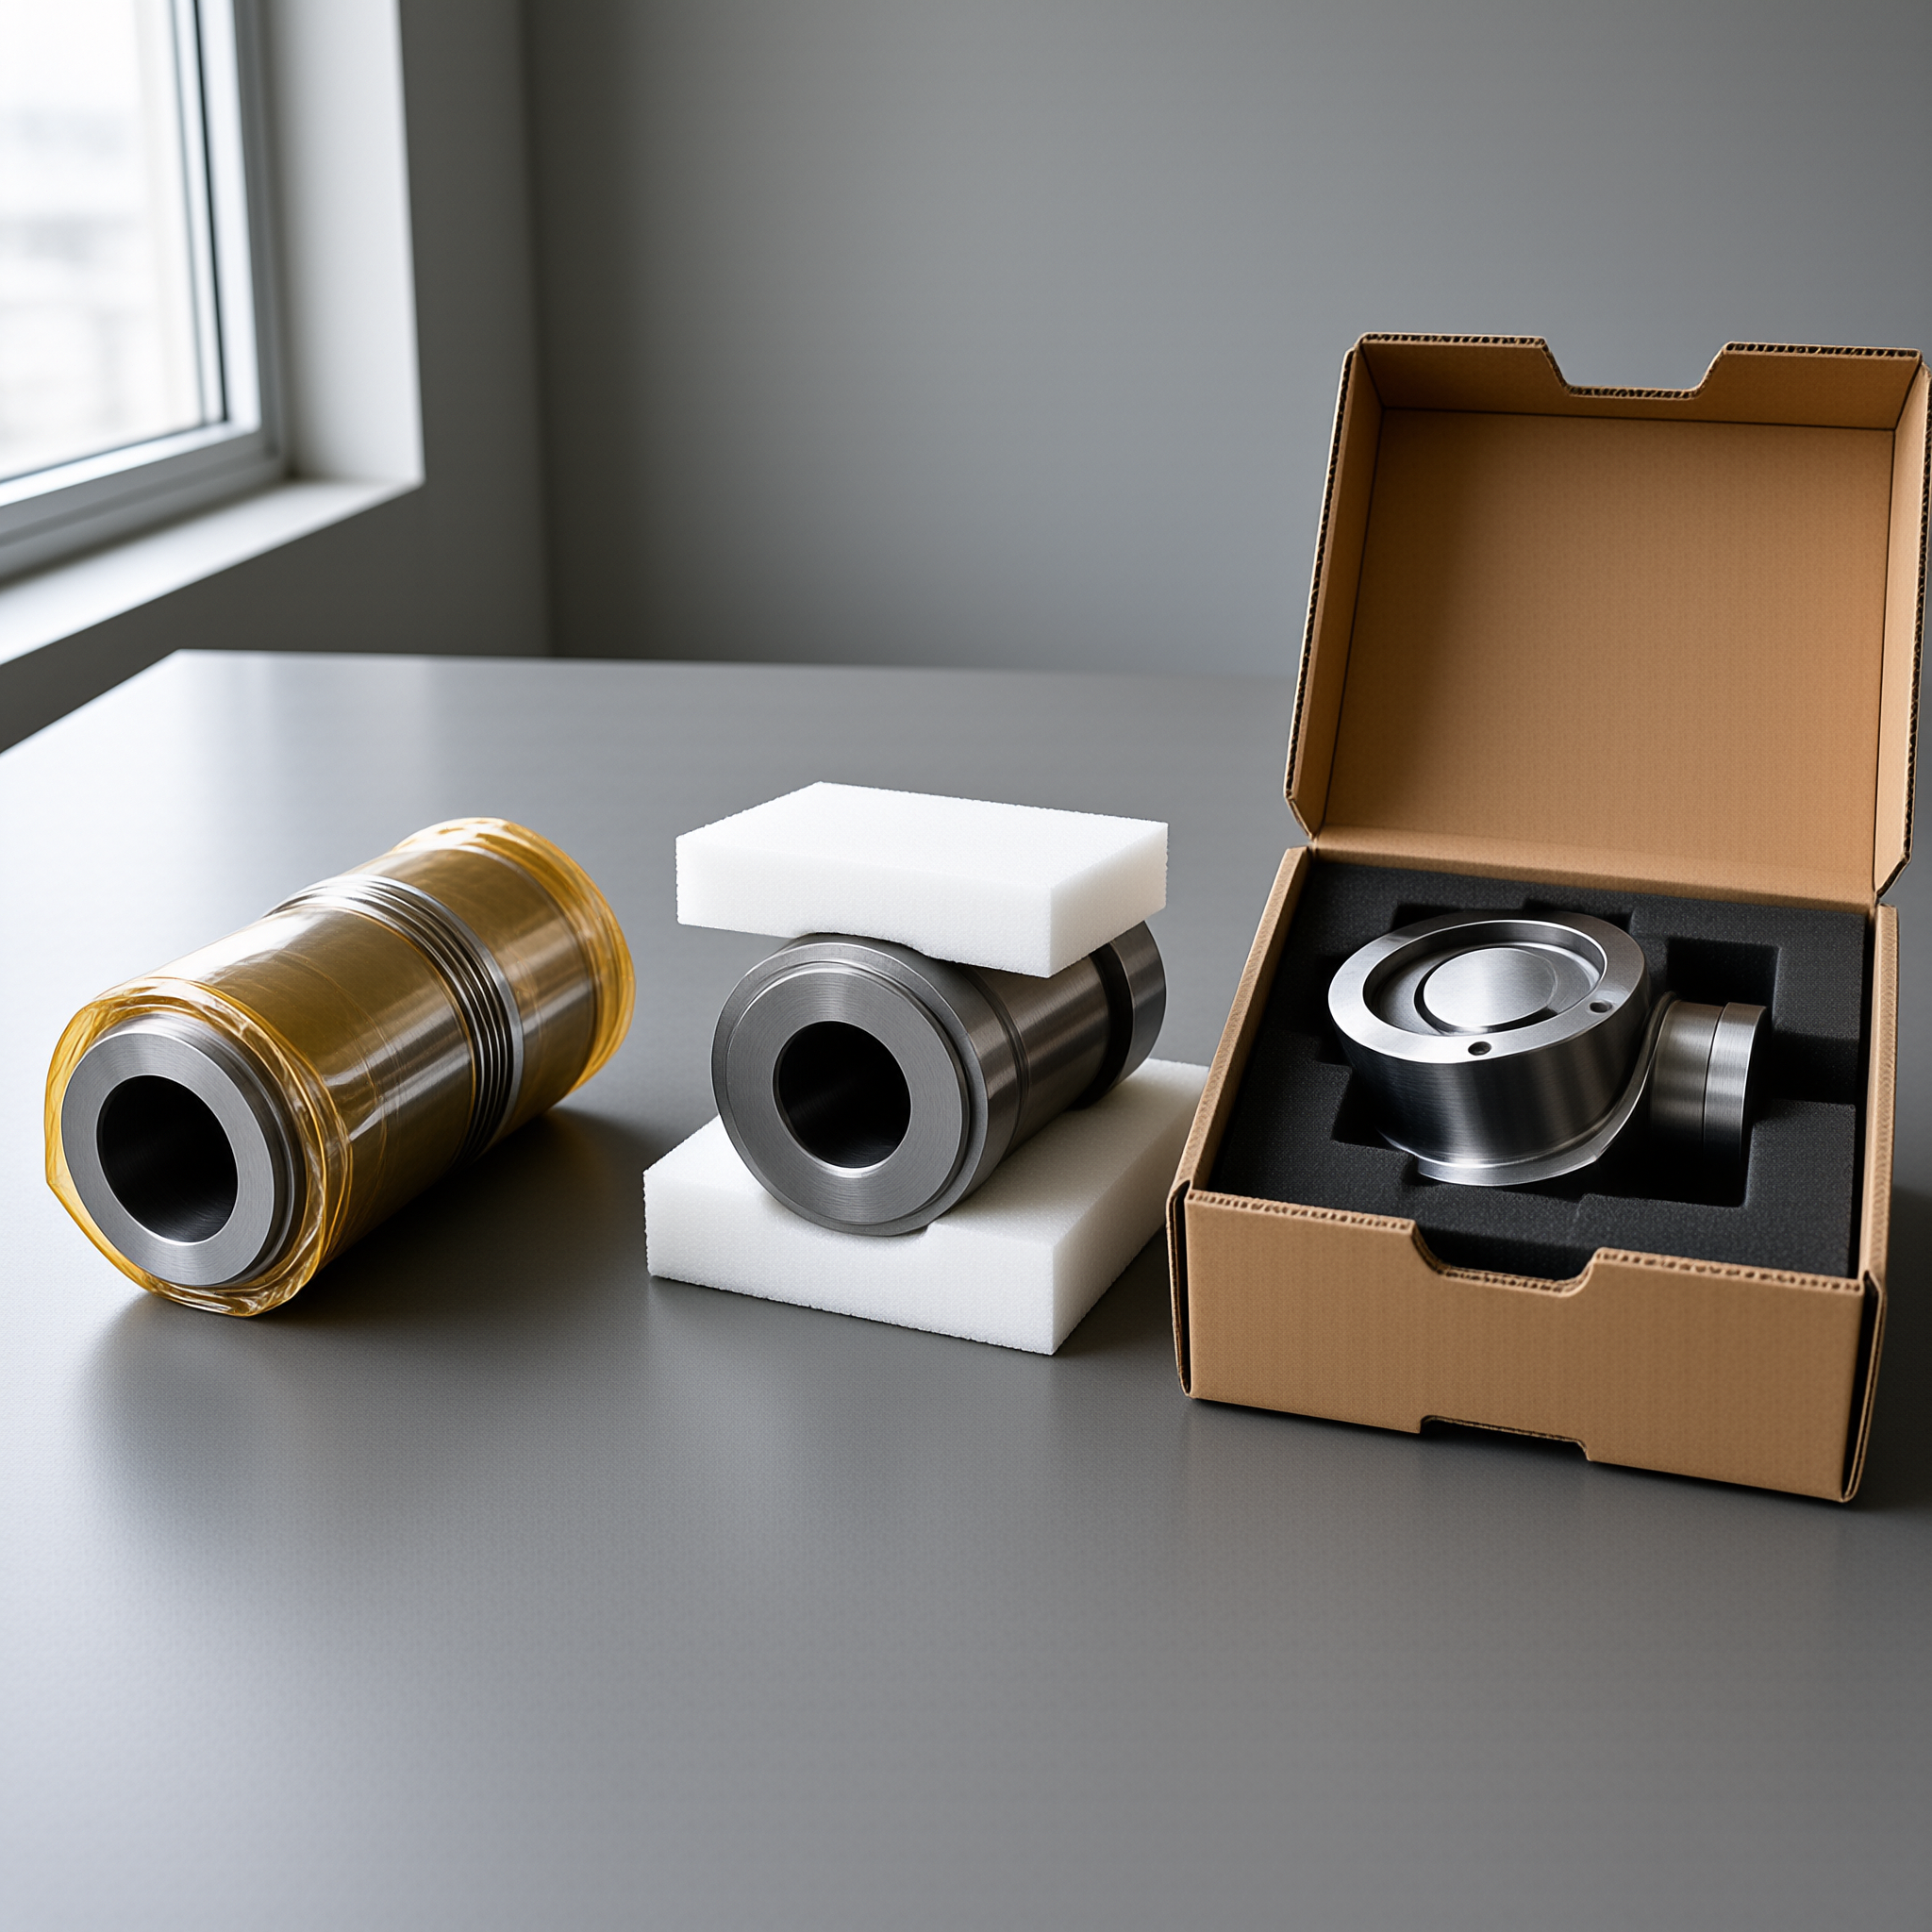
EPE foam interleaving carries most of the scratch protection metal parts shipping workload. Low-tack peel-coat film protects cosmetic-critical faces, and shaped foam liners hold parts away from the carton wall.
Foam works by separating two hard surfaces with a compliant layer that deforms under load. A 2 mm EPE sheet converts point contact between two machined edges into contact distributed across roughly 15-20 mm of surface. Peel-coat film adds protection directly on the finished face, but only while the adhesive stays below the tack level that leaves residue on anodised or polished surfaces.
In linear abrasion testing at 0.5 kg load, unprotected aluminium coupons showed visible scratching within 12 cycles. Coupons interleaved with 2 mm EPE foam showed no measurable surface damage after 500 cycles (internal observation; n=30 coupons, 1,000-grit polished surface, linear abrasion tester).
Two millimetres of EPE foam eliminated measurable surface damage across 500 abrasion cycles; unprotected aluminium scratched within 12.
| Method | What It Protects | Best For | Cost Index | Watch Out For |
|---|---|---|---|---|
| EPE foam interleaving | General machined faces and edges | Mixed-part cartons, burr-free edges | Low | Compression set above 0.5 kgf/cm² |
| Low-tack peel-coat film | Cosmetic and anodised faces | Visible critical surfaces | Medium | Adhesive residue if left on over 90 days |
| Foam-in-place cradles | Complex geometry, single heavy part | Low-volume, high-value components | High | Cure time adds 20-30 minutes per carton |
| Individual compartments | Part-to-part contact | Batches of identical small parts | Medium | Corrugated dividers alone are not shock protection |
Shock and Vibration Control: ISTA 3E vs ASTM D4169 Transit Testing
ISTA 3E is a performance test for packaged products moving through parcel and less-than-truckload distribution, including ocean legs. ASTM D4169 is a broader standard built from selectable distribution cycles matched to the actual shipping mode.
ISTA 3E applies a fixed sequence — random vibration, rotational edge drop, and concentrated impact — to a packaged unit. The sequence reproduces cumulative fatigue, the damage that builds over 30 days rather than in a single event. ASTM D4169 runs on the same principle but lets the user choose a distribution cycle, so a sea-freight profile can be combined with air or rail in one test plan.
ISTA 3E simulates 30+ days of ocean freight through vibration, shock and drop sequences on units up to roughly 150 lb (ISTA 3E-2017; standard-defined test sequence). ASTM D4169-22 defines 18 distribution cycles chosen by route, which is why exporters cite ASTM D4169 and ASTM B117 standards alongside ISO standards for packaging and transit testing when writing a transit-test specification. A passing ISTA 3E packaging test result is tied to one unit weight, foam density and carton geometry — change any of the three and the result does not carry over.
Container Loading Strategy: Blocking, Bracing, and ISPM 15 Compliance
Blocking stops cargo from moving; bracing transfers the remaining load into the container structure. Both are required, and any wood used must carry valid heat-treatment marking before the doors close.
A 20-foot container is rated for roughly 28 tonnes of static load, but its lashing points and side walls tolerate far less dynamic side force. When a stack shifts by even 50 mm, the gap multiplies at each layer and the upper cartons fall. Blocking limits movement at the base, and diagonal bracing converts lateral force into compression along the container wall.
Under ISPM 15 wood packaging rules, wood must be heat-treated to a 56°C core temperature for 30 minutes, or fumigated, then stamped with the IPPC mark including country code and producer registration (ISPM 15, FAO, 2019 revision). Non-compliant wood is fumigated, re-exported, or destroyed at destination. Buyers often compare pallet suppliers on unit price, but one refused container costs 20-40x the savings on unmarked pallets — the tradeoff is per-pallet cost against landed risk.
Choosing the Right Packaging System: A Cost vs Protection Decision Matrix
Packaging level should be set by three variables: component value, dimensional tolerance, and door-to-door transit duration. Matching those three against a protection tier takes ten minutes; optimising material cost in isolation takes weeks and usually ends in rework.
Low-Value Commodity Components
Standard fasteners, brackets and spacers justify corrosion control only. A VCI bag with 50 g desiccant per cubic foot inside a double-wall carton holds total packaging cost near 2-3% of part value.
Shock protection at this tier is a single layer of corrugated or 10 mm EPE. Foam-in-place cradles cost more than the parts are worth, and that spend is not recoverable.
High-Tolerance Aerospace or Medical Parts
Tolerances below ±0.02 mm and cosmetic-critical surfaces justify the full four-layer stack with individually serialised compartments.
Budget 7-9% of part value. Foam-in-place cradles, peel-coat film on every critical face, and a humidity indicator card inside each carton are baseline requirements at this tier, not optional extras.
Long-Haul Routes Over 30 Days
Transit longer than 30 days changes the desiccant calculation, not the layer count.
Roughly double the desiccant quantity per cubic metre for 30-45 day routes, and specify a 24-month-rated VCI film instead of a 12-month grade. On routes crossing the equator, add container desiccant poles outside the individual cartons to control ambient humidity at container level.
| Component Profile | Tolerance | Transit | Recommended machined parts packaging materials | Cost (% of part value) |
|---|---|---|---|---|
| Under $20, cosmetic not critical | ±0.1 mm | 20-30 days | VCI bag + desiccant + double-wall carton | 2-3% |
| $20-200, mixed surfaces | ±0.05 mm | 25-35 days | VCI bag + EPE interleaving + foam cradle + plywood crate | 4-6% |
| Over $200, cosmetic critical | Under ±0.02 mm | 30-45 days | VCI bag + peel-coat film + foam-in-place + ISPM 15 crate | 7-9% |
| Any value, high-humidity route | Any | Over 45 days | Above + container desiccant poles + 24-month VCI film | +1-2% |
Measure door-to-door transit days, then add 7-10 days for inland legs and customs dwell.
Check the largest unsupported span on the part — anything over 150 mm needs a cradle, not just foam.
Confirm the destination country's wood import rules before ordering pallets.
Set desiccant quantity from container volume, not from part quantity.
Re-validate the whole packaging configuration if part weight changes by more than 15%.
In the CNC component line we support, the validated packaging sequence is fixed at four stations: VCI bag insertion with desiccant, EPE foam cradle fitting, sealed-carton weight check, and ISPM 15-marked plywood crate assembly — every station is signed off on the traveller before crate closure (47 batches across 12 CNC supplier sites; internal packaging traveller audit, 2024).
Common Packaging Failures: Why Parts Still Arrive Damaged
Recurring damage almost always traces to five avoidable causes: a VCI bag punctured by a sharp machined burr, desiccant left exposed after the pouch was opened, foam cradles loaded past their compression rating, missing blocking between pallet stacks, and cartons stacked beyond their compression strength.
Each failure defeats one layer rather than the whole system, which is why the damage looks localised. A 3 mm puncture lets humidity through at that single point, so corrosion starts on the face nearest the opening. Foam loaded past 0.5 kgf/cm² takes a permanent compression set — a cradle measuring 40 mm at packing measures 32 mm at destination and no longer holds the part.
A Tier-2 automotive supplier in Germany ships 4,800 CNC-machined aluminium valve bodies per month to a Tier-1 assembly plant in Mexico, with 21-day average sea transit. Damage claims ran at 1.8% of shipments, dominated by surface scoring and edge corrosion. After switching to a four-layer system — VCI bag, 50 g desiccant, EPE foam cradle, ISPM 15 plywood crate — validated to ISTA 3E and ASTM B117, claims fell to 0.4% and packaging cost settled at 6.2% of finished part value. Across nine European CNC exporters with 12 months of claim records, machined parts damage during shipping averaged 1.5-3.0% before validation and dropped below 0.5% afterwards (industry observation, 2023-2024; n=9 exporters, internal claim log review).
Acceptance Criteria and Pre-Shipment Inspection Checklist
Acceptance happens at two points: the packaging station before the crate is closed, and the load port before the container doors are sealed. Both need a signed pre-shipment inspection checklist.
A checklist works because the failure modes are order-dependent. Desiccant goes in before the bag is sealed, and the carton weight check happens before the crate is closed. Reversing the sequence means opening a finished crate, which is where most packaging non-conformances get introduced.
In a 2024 traveller audit covering 47 batches across 12 CNC supplier sites, the sealed-carton weight check was the station most often skipped, and those crates were reopened at three times the rate of fully signed travellers (internal packaging traveller audit, 2024).
VCI bag seal integrity: heat-seal continuous, no puncture from burrs or sharp edges.
Desiccant activation date and quantity recorded against the route duration.
Foam cradle fit: no gaps over 2 mm, no compression set visible on recovered foam.
Carton weight check recorded and matched to the packing list.
Blocking and bracing installed, with no more than 50 mm of lateral movement at any stack.
IPPC stamp legible on every wooden component, with country code and producer number.
Humidity indicator card present and photographed before crate closure.
Frequently Asked Questions on Packaging Precision Machined Parts for Export
- What is the most effective packaging for precision machined parts in sea freight?
- A VCI barrier bag with 50 g desiccant per cubic foot, an EPE foam cradle, and an ISPM 15-marked plywood crate validated to ISTA 3E. This four-layer stack suits most finished components.
- How long does VCI protection last inside a sealed export crate?
- Typically 12-24 months in a sealed, dry barrier bag. For transit above 30 days, recalculate desiccant quantity rather than simply increasing film thickness.
- What is the difference between ASTM D4169 and ISTA 3E?
- ASTM D4169 covers 18 selectable distribution cycles across multiple transport modes. ISTA 3E is a fixed ocean and parcel-level protocol — many exporters run both for layered validation.
- Why do machined parts still corrode inside a sealed package?
- Three common causes: moisture ingress during container rain, thermal cycling that drives condensation, and VCI saturation beyond its roughly 30 cm effective radius from the film surface.
- Do I need ISPM 15-marked wood for export crates?
- Yes for most destinations. Heat treatment to a 56°C core for 30 minutes or fumigation, plus the visible IPPC stamp, is mandatory and verified at the destination port.
- How do I prevent scratches on polished metal surfaces during transit?
- Use 2 mm EPE foam interleaving, low-tack peel-coat film on critical faces, and individual compartments so parts cannot contact each other or the carton wall.
- How much does export-grade machined parts packaging add to unit cost?
- Typically 4-9% of finished part value. Cosmetic-critical, high-tolerance parts sit at the upper end; commodity fasteners can be protected for 2-3%.
Packaging at 4-9% of part value costs less than a 1.5-3% claim rate plus a line stoppage at the customer.
Packaging precision machined parts is ultimately a risk-pricing decision: pay 4-9% more per unit at the packaging station, or absorb 1.5-3% claim rates plus inbound quality holds and line stoppages at the customer. Teams building a specification from scratch should start with transit duration and tolerance class, select a protection tier from the decision matrix above, and validate the finished configuration against ISTA 3E before scaling it across a product family.


